





Overcoming Springback: How to Bend High-Tensile Steel with Precision
Release Time:
2025-11-24
Overcoming Springback: How to Bend High-Tensile Steel with Precision
In the evolving landscape of heavy metal fabrication, the materials we work with are changing. The industry is rapidly shifting away from standard mild steel toward high-tensile, wear-resistant steels such as Hardox, Weldox, Domex, and other ultra-high-strength grades. These materials offer incredible durability for dump trucks, excavators, and structural components, allowing for lighter and stronger designs.
However, for the press brake operator and the production manager, these materials present a significant, persistent challenge: Springback.
If you have ever attempted to bend a piece of high-strength steel to a perfect 90-degree angle, only to watch it relax back to 98 or 100 degrees as soon as the clamping pressure is released, you have battled springback. It is the single largest cause of inaccuracy, wasted material, and production delays in modern fabrication shops using HAVI CNC Machinery.
In this comprehensive guide, we will dismantle the science of springback, explain why standard bending formulas fail with these modern materials, and demonstrate how advanced CNC technology—specifically the WE67K Series—can turn this unpredictable variable into a precise, repeatable science.
Understanding the Physics: Why Does Springback Happen?

To control springback, one must first understand the internal mechanics of the metal during the bending process. When a press brake punch forces a metal plate into a die, the material undergoes two distinct types of stress simultaneously:
- Elastic Deformation: This is the temporary stretching of the material's molecular bonds. Think of this like a rubber band; when you pull it, it stretches, but when you let go, it snaps back to its original shape.
- Plastic Deformation: This is the permanent shifting of the material's structure. Once the stress exceeds the material's 'Yield Point,' it stays bent.
The phenomenon of springback occurs because, while you have achieved Plastic deformation to create the bend, the Elastic stress remains trapped in the bend zone. As soon as the punch retracts and the force is removed, that elastic energy is released. The material tries to return to its original flat shape, causing the bend angle to open up.
The High-Tensile Difference

Why is this such a massive issue for High-Tensile Steel compared to Mild Steel? The answer lies in the Yield Strength.
- Mild Steel (e.g., S235): Has a relatively low yield strength (~250 MPa). The ratio of elastic to plastic deformation is low, resulting in a manageable springback of usually 0.5° to 1°.
- High-Tensile Steel (e.g., Hardox 450): Has an extremely high yield strength (~1200 MPa). To bend it permanently, you must apply massive force to overcome that yield point. Consequently, the amount of stored elastic potential energy is significantly higher.
When bending these tough materials, it is not uncommon to see springback values of 10° to 20°, or even more depending on the radius. If your CNC Press Brake and operator are not prepared for this, you will never achieve a precise angle on the first try.
Why Standard Calculations and "Rules of Thumb" Fail
For decades, seasoned fabricators relied on mental math or simple charts to estimate over-bending. "If I want 90 degrees, I'll bend to 88." For mild steel, this worked. For high-tensile steel, this approach is a recipe for scrap metal.
Static formulas often fail because they cannot account for the subtle, invisible variables present in every batch of high-strength steel.
1. Yield Strength Inconsistency
Steel manufacturing is not perfect. A plate of Domex 700 labeled as having a 700 MPa yield strength might actually have 720 MPa in one batch and 690 MPa in another. Even a 5% variance in material strength can change the springback by several degrees. A standard calculator assumes the material is perfect; the reality is not.
2. Grain Direction Sensitivity
High-tensile steel has a distinct 'grain' created during the rolling process at the steel mill.
- Transverse Bending (Perpendicular to grain): This is the preferred method. The material is stronger and less likely to crack, but it requires more tonnage and has different springback characteristics.
- Longitudinal Bending (Parallel to grain): The material bends easier (less tonnage), but the springback is significantly different, and the risk of the plate cracking completely is very high.
3. The Radius-to-Thickness Ratio (R/T)

The relationship between your punch radius and the plate thickness is the biggest multiplier of springback. As the inner radius of the bend grows larger (relative to thickness), the springback increases drastically. Since high-tensile steel requires a larger radius to prevent cracking, you are forced into a geometry that naturally creates more springback.
Comparative Springback Data Table
To illustrate the severity of the difference, consider the approximate springback values required to achieve a final 90° angle using Air Bending methods:
Material Type | Tensile Strength (Approx.) | V-Die Opening (Rec.) | Springback (R/T = 1) | Springback (R/T = 5) |
Mild Steel (S235) | 360 - 510 MPa | 6x - 8x Thickness | 0.5° - 1.0° | 1.5° - 2.0° |
Stainless Steel (304) | 520 - 720 MPa | 8x Thickness | 1.0° - 2.0° | 2.5° - 3.5° |
High Strength (Strenx 700) | 780 - 930 MPa | 10x - 12x Thickness | 4.0° - 6.0° | 9.0° - 12.0° |
Wear Plate (Hardox 450) | 1400 MPa | 12x - 14x Thickness | 8.0° - 12.0° | 15.0° - 25.0° |
Note: These values are estimations. The exact value depends on the specific tooling geometry and the actual chemical composition of the sheet.
The Solution Part 1: Intelligent CNC Control (Delem Systems)
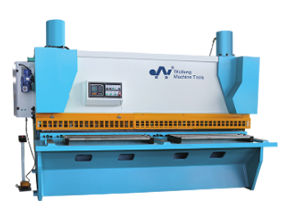
Since the physical properties of the steel prevent us from eliminating springback, we must predict it with extreme accuracy. This is where the difference between a standard torsion bar machine and a high-end WE67K Series Electro-Hydraulic Press Brake becomes apparent.
At HAVI CNC, we equip our WE67K series with advanced controllers, such as the Delem DA66T or DA58T. These are not just screens; they are powerful computers capable of managing the complex physics of bending.
The Database Driven Workflow
The Delem controller solves the springback equation through a data-driven approach:
- Material Library: The operator does not guess. They select the specific material (e.g., "Steel 1200 MPa") from the controller's library.
- Parameter Input: The operator inputs the thickness and the desired final angle.
- Automatic Calculation: The CNC calculates the "Deep Insertion" (Y-axis depth). It knows that to get 90°, it might need to push the ram down to an equivalent of 78°.
- Correction Database: This is the most critical feature. If the first bend results in 92° instead of 90°, the operator simply types "92" into the correction field. The Delem controller doesn't just fix that one bend; it saves that correction factor into its database. For every subsequent bend on that batch of steel, the machine automatically applies the precise compensation.
This capability transforms a process that used to require skilled intuition into a process of digital precision.
The Solution Part 2: Addressing the "Canoe Effect" with Crowning
Calculating the springback angle is only half the battle. The other challenge with high-tensile steel is ensuring the angle is consistent from the left side of the machine to the right side.
High-tensile steel requires massive tonnage—often 3 to 4 times more force than mild steel. When you apply 200 or 400 tons of force, the physical structure of the press brake (the upper ram and the lower bed) will deflect. The center of the machine naturally bows away from the pressure.
Without compensation, this results in the "Canoe Effect":
- The ends of the sheet (where the side frames are) receive full pressure and bend to 90°.
- The center of the sheet (where deflection is highest) receives less pressure and bends to 92° or 93°.
HAVI's Mechanical Crowning System
To process high-tensile steel, a Crowning System is not optional; it is mandatory.
The HAVI WE67K Series features an advanced CNC Automatic Mechanical Crowning System integrated into the lower worktable.
- Mechanism: Inside the worktable, a series of opposing wedges slide against each other.
- Function: As the wedges slide, they physically raise the center of the die by a fraction of a millimeter (creating a curve, or "crown").
- CNC Integration: This is not manual. The Delem DA66T controller calculates exactly how much the machine will deflect based on the programmed tonnage. It then commands the crowning motor to adjust the wedges automatically before the bend occurs.
The result is a perfectly straight bend, with consistent angles from end to end, regardless of the immense force being applied.
Step-by-Step Guide: Best Practices for Bending Hard Steel
If your shop is transitioning from general fabrication to heavy-duty high-tensile projects, specific protocols must be followed to protect both the machine and the operator.
1. Tooling Selection is Critical
Standard tooling is insufficient. The high surface pressure of Hardox can crush standard dies.
- Punch: Use punches with a large radius (minimum R3 to R6) to distribute the load.
- Die: Use V-dies with hardened rollers or hardened shoulders to prevent rapid wear.
- V-Opening: Always use a V-opening that is 10x to 12x the plate thickness. A tighter V-die increases tonnage drastically and can cause the plate to shatter.
2. Manage the Tonnage
Never exceed the concentrated load limit of your press brake. High-tensile steel builds tonnage very quickly.
Tip: If your machine is rated for 100 tons per meter, and you are bending a small 200mm bracket of thick Hardox, you might be applying 50 tons into that tiny area, damaging the tool or the beam. Always check the HAVI tonnage calculator.
3. Grain Direction Orientation
Whenever possible, design your parts so they can be bent transverse to the rolling direction (across the grain).
- This orientation allows for a tighter bend radius.
- It provides more consistent springback results.
- If you must bend parallel to the grain, increase your V-die opening and punch radius significantly to prevent cracking.
FAQ: High-Tensile Bending Queries
- Q: Can I use a standard WC67Y (Torsion Bar) Press Brake for Hardox?
A: While physically possible for rough work, it is highly discouraged for precision parts. A standard WC67Y Hydraulic Press Brake uses a torsion bar for synchronization, which lacks the independent Y1/Y2 cylinder control and the sophisticated database management required to handle the extreme springback of high-tensile steel. You will struggle with angle consistency. The Electro-Hydraulic WE67K Series is the industry standard for this application.
- Q: Why does the calculated springback change between two plates of the same thickness?
A: This is likely due to the "Delta Yield" issue. Two plates from different steel heats (batches) can have slightly different chemical compositions and rolling histories, leading to variances in Yield Strength. The CNC controller's "Teach" or "Correction" function is the best way to handle this.
- Q: Should I use Air Bending or Bottoming for high-tensile steel?
A: You must always use Air Bending. Never attempt to "Bottom Bend" or "Coin" high-tensile steel. The tonnage required to bottom bend these materials would be astronomical and would likely destroy your tooling and damage the machine frames. Air bending allows the CNC to control the angle via depth, which is the only safe method for these materials.
Conclusion
Bending high-tensile steel is no longer a "black art"—it is an engineering challenge that has been solved by technology. The unpredictability of springback and the immense forces required to form materials like Hardox mean that relying on manual calculations or outdated machinery is a strategy for inefficiency.
By leveraging the power of the HAVI WE67K CNC Press Brake, you are not just buying a machine; you are acquiring a solution that integrates:
- Delem CNC Intelligence: To calculate and compensate for springback automatically.
- Mechanical Crowning: To ensure your bends are straight and true, eliminating deflection errors.
- Heavy Duty Build: To withstand the rigorous demands of high-yield materials day in and day out.
Don't let difficult materials dictate your production quality. Equip your shop with the technology designed to master them.
Are you ready to tackle high-tensile projects with confidence? Contact HAVI CNC Team to discuss our heavy-duty press brake solutions and receive a custom tonnage consultation for your specific material needs.
Related News
NanTong HAVI CNC Machinery Co., Ltd.
Phone/WhatsApp: +86 17606524813
Address: Libao Development Area,HaiAn jiangsu China